AIENGINEAR CALCULATOR · FLOW MEASUREMENT
Quick answer: how do you calculate flow through a Venturi meter?
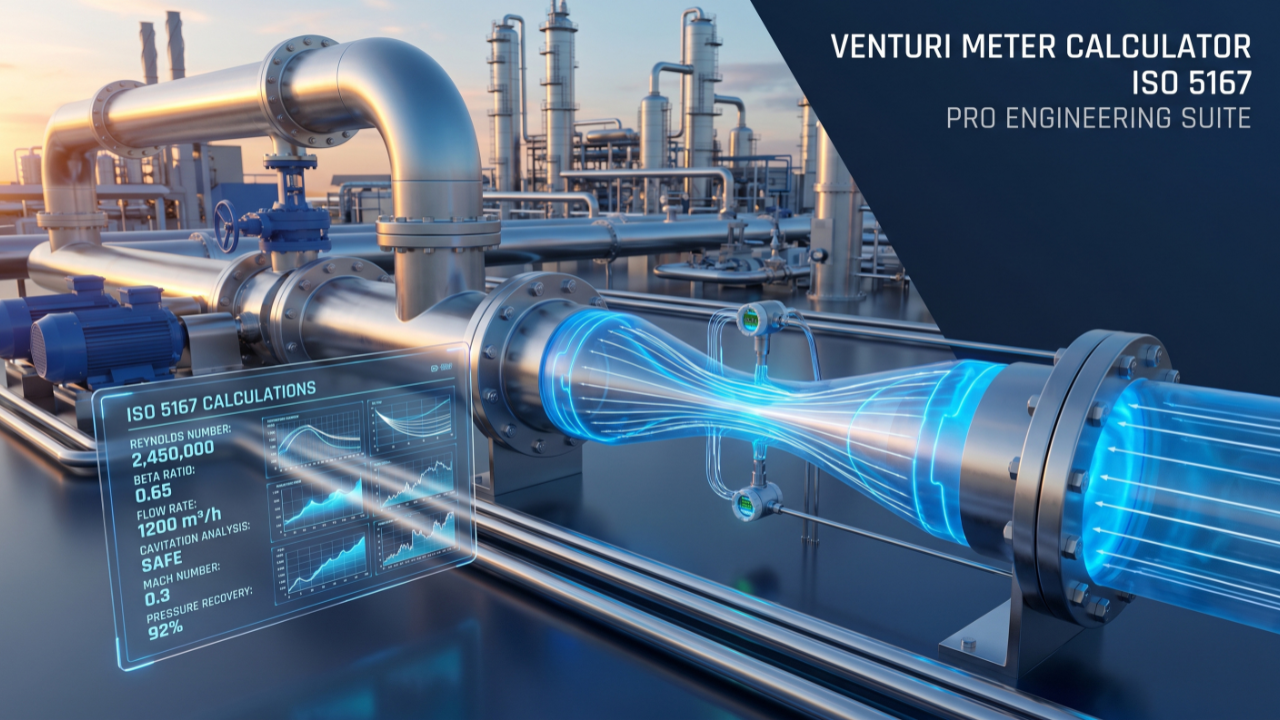
Measure the differential pressure Δp between the upstream tapping and the throat tapping, then apply the ISO 5167 mass-flow equation qm = (C / √(1 − β⁴)) · ε · (π/4) d² · √(2 Δp ρ₁). Here β = d/D is the diameter ratio, C the discharge coefficient (0.984 as-cast, 0.995 machined, 0.985 rough-welded below ReD = 10⁶), ε the expansibility factor (exactly 1 for liquids) and ρ₁ the upstream density. Because Δp grows with the square of flow, flow follows the square root of Δp. Enter your line size, fluid and differential above and the calculator returns mass flow, volumetric flow, velocities, Reynolds number, permanent loss, cavitation and choking margins and a full ISO GUM uncertainty budget.
Key takeaways
- A Venturi recovers most of the pressure it borrows: permanent loss is typically 5 % to 20 % of the differential, against 50 % to 80 % for an orifice plate at the same duty.
- ISO 5167-4:2022 is the current edition. Its headline technical change is a discharge coefficient of C = 1.000 with 1.8 % expanded uncertainty for machined convergent tubes above ReD = 10⁶, promoted from the informative annex into the body of the standard.
- Uncalibrated use is bounded: pipe bore 50 mm to 1 200 mm and ReD ≥ 2 × 10⁵, with tighter per-type limits on D, β and Re.
- Design β into the 0.4 to 0.7 band. Below that, throat velocity and cavitation risk climb; above it, the signal weakens and bore tolerances dominate the uncertainty.
- Turndown is no longer the old 3:1 rule of thumb. ISO 5167-1:2022 Annex D recognises that a modern transmitter can cover roughly 100:1 in differential pressure, about 10:1 in flow.
- Everything here runs in your browser. No inputs leave your device and nothing is stored.
How to use the calculator
The tool runs two ways round. In rating mode you know the geometry and the differential and want the flow. In sizing mode you know the flow you need to measure and want the throat diameter. Both use the same ISO 5167 equation, so the two agree to within rounding.
- Pick the fluid phase. Liquid, gas or steam. The phase decides whether the expansibility factor is applied and which warnings are active.
- Enter the line. Use the measured internal diameter if you have it. If not, choose the nominal size and schedule and let the tool look up the bore. Never use the nominal size as the bore: a 6-inch Schedule 40 pipe has a 154.08 mm bore, not 152.4 mm, and the difference moves β and the flow.
- Enter the fluid properties at operating conditions, not at standard conditions. Density and viscosity both shift with temperature, and the Reynolds number check depends on them.
- Choose the Venturi type. As-cast, machined or rough-welded sheet-iron. This sets the discharge coefficient, its uncertainty and the validity envelope.
- Enter the differential, or the target differential if sizing. A good starting target is a differential that gives a sensible transmitter span without pushing the permanent loss past what the pump or compressor can absorb.
- Read the compliance panel before the flow number. It states whether D, β and ReD are inside the ISO envelope for the type you selected. Outside it, the flow still computes but the standard uncertainty no longer applies.
- Check the margins. For liquids, the cavitation index. For gases and steam, the throat Mach number and the pressure ratio against the choking limit.
- Run the turndown check at minimum flow as well as maximum. The commonest sizing error is a meter that is perfect at design flow and below the Reynolds limit at turndown.
Practical tip
Size at the minimum flow first. The maximum flow sets the transmitter span, but the minimum flow is what decides whether the meter is usable, because that is where Reynolds number falls below the ISO limit and where the differential disappears into transmitter noise. If the minimum works, the maximum almost always does.
What is a Venturi meter?
A Venturi meter is a differential-pressure flow element: a deliberate, smoothly profiled constriction in the pipe, with pressure tappings before it and at its narrowest point. Giovanni Battista Venturi described the underlying effect in 1797, and Clemens Herschel turned it into a practical commercial meter in the 1880s. The geometry has barely changed since, which is a fair indication of how well it works.
The element has three parts. A converging entrance cone, typically 21 degrees included angle, accelerates the fluid. A short cylindrical throat holds it at peak velocity and carries the downstream tapping. A long diverging outlet cone, typically 7 to 15 degrees, decelerates it again. That final cone is the whole point of the device: a gentle expansion keeps the flow attached to the wall instead of separating into a turbulent jet, so most of the kinetic energy gained in the throat is handed back as static pressure rather than dissipated as heat.
Two conservation laws do the work. Continuity says mass flow is the same at every cross-section, so a smaller area forces a higher velocity. Bernoulli says that along a streamline the sum of static and dynamic pressure is conserved, so the velocity rise must be paid for with a static-pressure fall. The meter senses that fall. Because dynamic pressure scales with velocity squared, the differential scales with flow squared, and flow therefore scales with the square root of the differential. That square-root relationship governs everything downstream of the element: transmitter sizing, turndown, low-flow cut-off, and the single most common commissioning error in differential-pressure metering.
The ISO 5167 flow equation
Begin with Bernoulli between the upstream section 1 and the throat 2, assuming an incompressible, frictionless, one-dimensional flow:
Continuity gives v₁A₁ = v₂A₂, and since area scales with diameter squared, v₁ = v₂β². Substituting and solving for the throat velocity:
Two corrections turn this ideal result into the equation the standard actually uses. The discharge coefficient C absorbs everything the ideal derivation left out: boundary-layer growth on the convergent wall, the non-uniform velocity profile, and the small frictional loss between the tappings. The expansibility factor ε accounts for a compressible fluid becoming less dense as it accelerates into the throat. The result is the ISO 5167-1 working equation, common to every element in the series:
The group E = 1/√(1 − β⁴) is called the velocity-of-approach factor. It corrects for the fact that the fluid is already moving as it reaches the throat, and it is the reason β matters so much: at β = 0.4 it is only 1.013, but at β = 0.75 it reaches 1.19.
Volumetric flow follows as qv = qm/ρ, evaluated at whichever conditions you want to report. For gases this is where most arithmetic errors creep in, because actual, normal and standard volumes differ by a factor that depends entirely on the reference state you chose. The calculator reports all three and labels the reference conditions on each.
Venturi flow equation symbols and units
Aienginear Table 1
Venturi flow equation symbols and units
Every quantity in the ISO 5167 mass-flow equation, with SI units and typical values
| Symbol | Quantity | SI unit | Notes and typical range |
|---|---|---|---|
qₘ | Mass flow rate | kg/s | The primary result; multiply by 3600 for kg/h |
qᵛ | Volumetric flow rate | m³/s | qₘ/ρ at the stated reference conditions |
C | Discharge coefficient | – | 0.984 to 1.000 for classical Venturi tubes |
ε | Expansibility factor | – | Exactly 1 for liquids; 0.95 to 1.00 for gases |
β | Diameter ratio d/D | – | Design into 0.4 to 0.7; ISO limits are type-dependent |
E | Velocity-of-approach factor | – | 1/√(1 − β⁴); 1.013 at β=0.4, 1.19 at β=0.75 |
d | Throat diameter | m | At working temperature; apply thermal expansion if hot |
D | Pipe internal diameter | m | Measured bore, never the nominal size |
Δp | Differential pressure | Pa | Upstream tapping minus throat tapping |
ρ₁ | Upstream fluid density | kg/m³ | At operating pressure and temperature |
μ | Dynamic viscosity | Pa·s | Needed only for the Reynolds number check |
Reᶠ | Pipe Reynolds number | – | ρVD/μ; must be ≥ 2×10⁵ for uncalibrated use |
κ | Isentropic exponent | – | 1.4 air, ~1.3 natural gas, ~1.135 saturated steam |
Z | Compressibility factor | – | 1.0 at low pressure; 0.85 to 0.95 for gas at 40 to 100 bar |
Δω | Permanent pressure loss | Pa | Typically 5 % to 20 % of Δp |
Discharge coefficient C
The discharge coefficient is the ratio of real flow to the ideal flow the frictionless derivation predicts. For a classical Venturi tube it is remarkably high and, in the working range, essentially constant with Reynolds number. That constancy is the Venturi’s quiet advantage. A smooth contraction keeps the boundary layer thin and attached, so there is no vena contracta to speak of and almost no separation. An orifice plate, by contrast, forces the jet to separate at a sharp edge and contract downstream, which is why its coefficient sits near 0.6 and varies measurably with Reynolds number.
ISO 5167-4 does not give one coefficient. It gives three, one per manufacturing method, each with its own validity envelope and its own uncertainty. Choosing the wrong row is a common and expensive mistake, because the envelopes differ by more than the coefficients do.
ISO 5167-4 classical Venturi tube types, limits and coefficients
Aienginear Table 2
ISO 5167-4 classical Venturi tube types, limits and coefficients
Validity envelope for uncalibrated use, by convergent manufacturing method
| Convergent type | Pipe bore D | β range | Reᶠ range | C | U(C) at k=2 | Where it is used |
|---|---|---|---|---|---|---|
| As-cast | 100 to 800 mm | 0.30 to 0.75 | 2×10⁵ to 2×10⁶ | 0.984 | 0.7 % | Large water and utility mains; lowest uncertainty of the three |
| Machined | 50 to 250 mm | 0.40 to 0.75 | 2×10⁵ to 1×10⁶ | 0.995 | 1.0 % | Small and medium process lines; the most common type |
| Machined, high Re | 50 to 250 mm | 0.40 to 0.75 | > 1×10⁶ | 1.000 | 1.8 % | New in the body of ISO 5167-4:2022; common in high-pressure gas |
| Rough-welded sheet-iron | 200 to 1200 mm | 0.40 to 0.70 | 2×10⁵ to 2×10⁶ | 0.985 | 1.5 % | Large fabricated elements where casting or machining is impractical |
| Flow-calibrated | As calibrated | As calibrated | As calibrated | Certificate | 0.1 to 0.5 % | Custody transfer and anywhere the uncalibrated uncertainty is too wide |
Read the envelope, not just the coefficient
Note that the machined type has the highest coefficient but the narrowest bore range, and that the as-cast type has the lowest uncertainty of the three at 0.7 %. Operating outside a type’s envelope does not stop the equation working; it means the stated uncertainty on C no longer applies, and ISO 5167-4 Annex B directs that the uncertainty on C be doubled when β exceeds the permitted maximum. The calculator flags every excursion rather than silently returning a confident-looking number.
What changed in ISO 5167:2022
The whole ISO 5167 series was revised in 2022, the first comprehensive update since the 2003 restructure. Most of the changes are harmonisation across the parts, but several affect how a Venturi is specified and how its uncertainty is reported. If your in-house sizing spreadsheet dates from before 2022, these are the points to check.
- A new coefficient at high Reynolds number. For machined convergent Venturi tubes above ReD = 106, the standard now gives C = 1.000 with a 1.8 % expanded uncertainty, moved from informative Annex B into the body of the standard. This matters most in high-pressure gas, where ReD above 106 is routine and the old approach was to stop at the 106 limit or extrapolate informally. Values at or below 106 are unchanged from 2003.
- Single pressure tappings are now permitted. Previously the standard assumed multiple tappings into a piezometer ring. Recognising long-standing practice in high-pressure gas metering, single tappings are now allowed where the upstream pipe is long and the tappings are well made, though longer straight lengths may be required.
- Uncertainty is stated in GUM language. What earlier editions simply called “uncertainty” is now explicitly the relative expanded uncertainty at a coverage factor k = 2. The numeric values did not change, but reports that quote a bare percentage without stating the coverage factor are now clearly incomplete.
- Turndown is addressed directly. ISO 5167-1:2022 Annex D recognises that a modern transmitter can cover roughly 100:1 in differential pressure, which is about 10:1 in flow, overtaking the old 3:1 rule of thumb that still circulates widely.
- Flow-calibration rules are explicit. Section 7 of Parts 2 to 6 now sets out how a calibrated element is to be handled, which previously varied between parts.
- Permanent loss is compared across the family. Annex F of Part 1 compares permanent pressure losses of the different primary elements; the Venturi has the lowest.
- Installation wording is clarified. Clause 6.2.8 on spacing with multiple fittings was reworded in Parts 2 to 4, and Part 1 clause 7.3 relaxes the practical burden of the “5 % 2°” flow-condition rule for sufficiently small β.
Why the turndown change matters
The familiar claim that a differential-pressure meter gives only 3:1 or 4:1 turndown comes from the era of analogue transmitters, where a 100:1 differential span was genuinely unusable at the bottom. Modern digital transmitters with good low-end accuracy and proper low-flow cut-off change the arithmetic. Annex D of Part 1 is worth reading before you specify dual transmitters in split range on the assumption that a single one cannot cope.
Expansibility for gas and steam
A liquid passes through a Venturi at effectively constant density, so ε = 1 exactly and there is nothing to correct. A gas does not. As it accelerates into the throat its pressure falls, and with it the density, so the real mass flow is slightly less than a constant-density calculation would suggest. The expansibility factor is that correction.
For Venturi tubes and nozzles, ISO 5167 uses a theoretical expansibility derived from isentropic expansion, not the empirical linear expression used for orifice plates. The factor depends on the pressure ratio τ = p₂/p₁, on the isentropic exponent κ and on β. It equals 1 when τ = 1, and falls as the differential grows and as β rises.
Two practical limits follow. First, the correlation is valid only for τ ≥ 0.75. Below that the standard does not support the expansibility, and the calculator blocks the result rather than reporting a number it cannot stand behind. Second, the expansibility carries its own uncertainty, which grows with both β and the pressure ratio and must be carried into the budget alongside the uncertainty on C.
In practice τ is rarely the binding constraint on a well-sized gas Venturi, because a differential large enough to push τ below 0.75 would also mean an unacceptable permanent loss. If your sizing is heading that way, the pipe is too small or the differential target is too ambitious.
Choosing the beta ratio
If there is one number that decides whether a Venturi installation is a pleasure or a nuisance, it is β. It sets the signal you get, the energy you lose, the velocity in the throat, and how severely a manufacturing tolerance on the bores propagates into the flow reading. Those four pull in different directions, which is why the useful range is narrower than the range the standard permits.
The sensitivity point is the one most often missed. Differentiating the flow equation shows that the relative sensitivity of flow to throat diameter is 2 + 2β⁴/(1 − β⁴). At β = 0.4 that is 2.05, so a 0.1 % error on d gives 0.2 % on flow. At β = 0.75 it rises to 2.99, and the error is half as large again. Meanwhile the signal is shrinking, so the transmitter contribution is growing at the same time. High β is efficient and unforgiving.
Beta ratio selection guide
Aienginear Table 3
Beta ratio selection guide
How the differential, permanent loss, throat velocity and bore sensitivity move with β
| β | E = 1/√(1−β⁴) | Throat velocity × pipe velocity | Flow sensitivity to throat bore | Signal strength | Permanent loss | Verdict |
|---|---|---|---|---|---|---|
| 0.30 | 1.004 | 11.1× | 2.02 | Very strong | Highest | As-cast only; high throat velocity, watch cavitation and erosion |
| 0.40 | 1.013 | 6.25× | 2.05 | Strong | Higher | Lower edge of the common band; robust against bore tolerance |
| 0.50 | 1.032 | 4.00× | 2.13 | Good | Moderate | A safe default when nothing else constrains the design |
| 0.60 | 1.070 | 2.78× | 2.31 | Moderate | Lower | Good balance of signal and energy; very common in process lines |
| 0.70 | 1.144 | 2.04× | 2.62 | Weaker | Low | Energy-efficient; bore accuracy and transmitter quality now matter |
| 0.75 | 1.194 | 1.78× | 2.99 | Weakest | Lowest | Upper ISO limit; tolerance-critical, specify and verify bores carefully |
Sizing a Venturi
Sizing runs the equation backwards. You know the flow you must measure, the fluid, the line size and roughly the differential you want; you need the throat diameter. There is no closed-form inverse because β appears both in the area term and inside E, so the tool brackets the answer and converges by bisection, then runs the result forward again to confirm it reproduces the target flow.
- Fix the pipe bore from the line specification, using the measured or schedule internal diameter.
- Choose a target differential. Something in the 25 to 100 kPa band suits most industrial transmitters and keeps the permanent loss modest. Let the available pump or compressor margin set the ceiling.
- Solve for d and β. If β lands outside 0.4 to 0.7, change the differential before you change anything else: lowering the target differential raises β, raising it lowers β.
- Check ReD at minimum flow. This is the binding constraint more often than anything else. If ReD at turndown falls below 2 × 10⁵, the uncalibrated coefficient no longer carries its stated uncertainty, and you need either a calibration or a different element.
- Check the throat. For liquids, confirm the throat pressure stays clear of the vapour pressure with margin. For gases and steam, confirm the throat Mach number stays below 0.3 and the pressure ratio well above both 0.75 and the critical ratio.
- Check the permanent loss against the available head, and price it over the plant life. On a large continuous duty this often dominates the whole economic case.
- Confirm the type envelope. A 300 mm line rules out a machined convergent under the uncalibrated rules; a 60 mm line rules out as-cast and rough-welded.
- Iterate. Two or three passes usually settle it. The calculator keeps each pass as a scenario so you can compare them side by side.
Installation and straight lengths
A Venturi is more tolerant of a disturbed velocity profile than an orifice plate, because the converging cone accelerates and partly re-organises the flow before it reaches the throat tapping. Tolerant is not immune. ISO 5167-4 sets required upstream straight lengths as multiples of D, varying with β and with the fitting immediately upstream, and gives two columns: one for zero additional uncertainty, and a shorter one that costs an extra 0.5 % on the flow.
Indicative upstream straight lengths for classical Venturi tubes
Aienginear Table 4
Indicative upstream straight lengths for classical Venturi tubes
Multiples of D, shown as zero-additional-uncertainty / 0.5 %-additional-uncertainty
| Fitting immediately upstream | β = 0.30 | β = 0.50 | β = 0.60 | β = 0.75 |
|---|---|---|---|---|
| Single 90° bend | 8 / 3 | 9 / 3 | 10 / 3 | 16 / 8 |
| Two or more 90° bends, any planes | 8 / 3 | 10 / 3 | 10 / 3 | 22 / 8 |
| Reducer 1.33D to D over 2.3D | 4 | 4 | 4 | 4 |
| Reducer 3D to D over 3.5D | 2.5 | 5.5 / 2.5 | 8.5 / 2.5 | 11.5 / 3.5 |
| Expander 0.67D to D over 2.5D | 4 | 4 / 5 | 6 / 4 | 7 / 6 |
| Expander 0.75D to D over D | 2.5 | 2.5 | 3.5 / 2.5 | 6.5 / 4.5 |
| Full-bore ball or gate valve, fully open | 2.5 | 3.5 / 2.5 | 4.5 / 2.5 | 5.5 / 3.5 |
| Downstream of the throat tapping | Fittings at least 4d beyond the throat tapping plane do not affect accuracy | |||
Short on straight pipe?
Three options, in order of preference. Lower β, because the requirement falls sharply below 0.6 and barely moves between 0.3 and 0.6. Accept the 0.5 % column and record it explicitly in the uncertainty budget, which is an honest trade rather than a fudge. Or fit a flow conditioner, bearing in mind it introduces its own permanent loss and must itself be installed to the conditioner’s compliance requirements.
Impulse lines and tappings
More differential-pressure measurements are ruined by the impulse system than by the primary element. The element is a piece of precision metalwork that holds its geometry for decades; the impulse lines are two small tubes that have to stay symmetric, full of the right fluid and free of blockage, in a plant that is doing its best to interfere with all three. The governing rule is simple: both legs must be identical in length, bore, routing, elevation and temperature. Any asymmetry produces a static-head difference that the transmitter cannot distinguish from real flow.
Impulse line and tapping rules by fluid phase
Aienginear Table 5
Impulse line and tapping rules by fluid phase
Tapping orientation, slope and accessories for liquid, gas and steam service
| Item | Liquid | Gas | Steam |
|---|---|---|---|
| Tapping position on the pipe | Side, or below the horizontal centreline | Top, or above the centreline | Side, at the horizontal centreline |
| Transmitter position | Below the tappings | Above the tappings | Below the seal pots |
| Impulse line slope | Down to the transmitter, so gas rises back to the line | Up to the transmitter, so condensate drains back | Down from the seal pots |
| Minimum slope | 1 in 12 | 1 in 12 | 1 in 12 |
| Accessories | Vent pots at high points | Drain pots at low points | Condensate seal pots at equal elevation on both legs |
| Fill medium | Process liquid | Dry gas | Condensate, equal level both legs |
| Dominant failure mode | Gas pocket in one leg reads low | Condensate in one leg reads high | Unequal condensate level gives a false zero |
| Freezing risk | Trace and insulate both legs equally | Usually none | Trace and insulate both legs equally |
| Manifold | Three-valve or five-valve manifold; equalise before zeroing, never leave the equaliser cracked open | ||
Uncertainty budget
A flow figure without an uncertainty is an opinion. The calculator builds a budget following the ISO Guide to the Expression of Uncertainty in Measurement: each input contributes a standard uncertainty, each is multiplied by a sensitivity coefficient derived analytically from the flow equation, the contributions are combined in quadrature, and the result is expanded by a coverage factor k = 2 for roughly 95 % confidence. The sensitivity coefficients are not assumed; they are differentiated from the equation and cross-checked numerically against finite differences.
The relative sensitivity coefficients are worth knowing by heart, because they tell you where to spend effort:
Two things follow. Tightening the differential-pressure measurement has only half the leverage you might expect, because its coefficient is 0.5. And the throat diameter has more than double leverage, so a bore tolerance that looks trivial on a drawing is not trivial in the budget. The worked budget below is for the water example in section 17.
Worked uncertainty budget: 6-inch water Venturi
Aienginear Table 6
Worked uncertainty budget: 6-inch water Venturi
Machined convergent, β = 0.584, combined by root-sum-square to ISO GUM
| Contribution | Sensitivity cᵢ | Std uncertainty uᵢ | Contribution cᵢuᵢ | Share of variance |
|---|---|---|---|---|
| Discharge coefficient C (machined, 1.0 % at k=2) | 1.000 | 0.500 % | 0.500 % | 75.1 % |
| Throat diameter d | 2.264 | 0.100 % | 0.226 % | 15.4 % |
| Differential pressure Δp | 0.500 | 0.250 % | 0.125 % | 4.7 % |
| Fluid density ρ₁ | 0.500 | 0.200 % | 0.100 % | 3.0 % |
| Pipe bore D | −0.264 | 0.300 % | 0.079 % | 1.9 % |
| Expansibility ε (liquid, exactly 1) | 1.000 | 0.000 % | 0.000 % | 0.0 % |
| Combined standard uncertainty uᶜ | – | – | 0.577 % | 100 % |
| Expanded uncertainty U at k = 2 | – | – | 1.15 % | ~95 % confidence |
Permanent loss and energy cost
The differential a Venturi produces is borrowed, not spent. Most of it comes back in the divergent cone. What does not come back is the permanent pressure loss Δω, and that is a real, continuous, lifetime operating cost paid by whatever is pushing the fluid.
For a classical Venturi tube the permanent loss is typically 5 % to 20 % of the differential, depending mainly on the divergent half-angle and the surface finish. A long, gentle divergent recovers better than a short, steep one; a smooth bore recovers better than a rough one. ISO 5167-4 treats permanent loss as design guidance rather than a single closed-form value, and this suite follows the standard in labelling it indicative. For an orifice plate the same duty costs 50 % to 80 %, and that gap is the whole commercial argument for the Venturi.
Annual pumping cost of permanent loss: 400 m³/h water at Δp = 50 kPa
Aienginear Table 7
Annual pumping cost of permanent loss
400 m³/h water, Δp = 50 kPa, 70 % pump efficiency, 8 760 h/yr, 0.12 per kWh
| Primary element | Δω / Δp | Δω | Shaft power | Energy per year | Cost per year |
|---|---|---|---|---|---|
| Classical Venturi, well-made divergent | 10 % | 5.0 kPa | 0.79 kW | 6 950 kWh | 834 |
| Classical Venturi, upper band | 20 % | 10.0 kPa | 1.59 kW | 13 900 kWh | 1 669 |
| Venturi nozzle | 25 % | 12.5 kPa | 1.98 kW | 17 380 kWh | 2 086 |
| Orifice plate, β = 0.6 | 65 % | 32.5 kPa | 5.16 kW | 45 190 kWh | 5 423 |
| Orifice plate, β = 0.5 | 75 % | 37.5 kPa | 5.95 kW | 52 140 kWh | 6 257 |
| Saving, well-made Venturi vs β=0.6 orifice | – | 27.5 kPa | 4.37 kW | 38 240 kWh | 4 589 |
Scale that up. The saving above is on one 6-inch line. On a 36-inch water transmission main or an LNG compression train, the recovered pressure is measured in hundreds of kilowatts, and the Venturi repays its higher purchase and installation cost within the first years of operation. That calculation, not the base accuracy, is usually what decides a Venturi against an orifice.
Cavitation in liquid service
The throat is the lowest-pressure point in the system. If the static pressure there reaches the liquid’s vapour pressure at the operating temperature, the liquid flashes. The bubbles are then carried into the divergent cone, where the pressure recovers and they collapse, violently and very close to the metal surface. The results are pitting of the throat and divergent, a rising noise level, a drifting reading as the geometry erodes, and eventually a meter that needs replacing.
The calculator computes the throat static pressure directly and reports a cavitation margin against the vapour pressure at the stated temperature. Incipient cavitation is approached as that margin closes. A Venturi is more forgiving than an orifice here, because the throat pressure is a broad minimum that recovers gently rather than the sharp vena-contracta minimum behind an orifice plate, but forgiving is not immune.
When to take cavitation seriously
Hot water close to its boiling point; light hydrocarbons, LPG and other volatile liquids; any liquid at low line pressure; suction-side installations; and any design pushed to a high differential to get a strong signal. The three remedies, in order of ease: raise the line pressure, reduce the differential by enlarging the throat, or move to a lower β. Raising the differential to improve the signal is exactly the wrong move on a marginal duty.
Choked flow and Mach number
A compressible fluid has an upper limit. As the differential grows, the throat velocity grows, and when it reaches the local speed of sound the throat chokes: mass flow stops responding to further differential, and the differential-pressure method simply stops working. Choking occurs when the throat pressure ratio falls to the critical value:
In practice the binding limit arrives long before choking. Two constraints bite first: the expansibility correlation is only valid for τ ≥ 0.75, and compressibility effects grow once the throat Mach number passes about 0.3, widening the uncertainty well before anything dramatic happens. The calculator reports the pressure ratio, the critical ratio, the throat Mach number and the choked-flow ceiling, and warns as Mach 0.3 is approached rather than waiting for sonic conditions.
Steam measurement
Metering steam with a Venturi is entirely practical provided the steam is single-phase: dry saturated or, better, superheated. The suite derives steam density from a saturated-steam correlation with a superheat correction, which tracks published steam tables closely across the common industrial range, and applies the compressible treatment with κ near 1.135 for saturated and around 1.3 for highly superheated steam.
Wet steam is out of scope and the tool says so. Suspended liquid droplets carry mass that a single-phase calculation ignores, so a wet-steam measurement will read low by an amount that depends on the dryness fraction. Measuring wet steam properly needs a two-phase method and a separate determination of dryness; treating it as dry saturated steam and accepting the answer is one of the more expensive mistakes in utility metering.
Steam also places the heaviest demands on the impulse system. Condensate seal pots must sit at equal elevation on both legs, both legs must be traced and insulated identically, and the transmitter must sit below the pots. An imbalance of a few centimetres of condensate produces a static-head error indistinguishable from a genuine differential, and it will quietly bias every reading until someone notices.
Turndown and rangeability
The square-root law sets the character of the problem. At 50 % of maximum flow the differential is 25 % of full scale; at 10 % flow it is 1 %. The usable turndown is therefore decided not by the Venturi but by how accurately the transmitter can measure the bottom of its span.
This is where received wisdom has fallen behind the standard. The familiar 3:1 or 4:1 figure comes from analogue transmitters, where the bottom of a 100:1 differential span was genuinely unusable. ISO 5167-1:2022 Annex D now recognises that a single modern transmitter can cover roughly 100:1 in differential pressure, which is about 10:1 in flow. If your specification still assumes 3:1 and reaches straight for dual transmitters in split range, it is worth re-reading that annex before adding hardware.
What has not changed is the need for a sensible low-flow cut-off, and the rule that square-root extraction happens in exactly one place in the loop. Configure it in the transmitter or in the control system, never both. Doing it twice raises the signal to the fourth root instead of the square root, and the resulting error is large, systematic, and surprisingly easy to live with for months before anyone questions the totaliser.
Worked examples
Example 1: water in a 6-inch line
Water at 20 °C, density 998 kg/m³, viscosity 1.002 mPa·s, in a 6-inch Schedule 40 pipe of 154.08 mm bore, at 6 bar gauge. A machined classical Venturi tube with a 90 mm throat gives β = 0.584, so E = 1.0638. The convergent is machined, so C = 0.995 and ε = 1 exactly. The measured differential is 50 kPa.
Example 1 results: 154.08 mm bore, 90 mm throat, Δp = 50 kPa
Aienginear Table 8
Example 1 results: water through a 6-inch machined Venturi
Every intermediate step, so you can check the calculator against hand working
| Quantity | Value | How it is obtained |
|---|---|---|
| Diameter ratio β | 0.5841 | 90 / 154.08 |
| Velocity-of-approach factor E | 1.0638 | 1/√(1 − 0.5841⁴) |
| Throat area A₂ | 0.006362 m² | (π/4) × 0.090² |
| Discharge coefficient C | 0.995 | ISO 5167-4, machined convergent |
| Expansibility ε | 1.000 | Liquid, exactly 1 |
| Mass flow qₘ | 67.27 kg/s | C·E·ε·A₂·√(2Δpρ) = 242.2 t/h |
| Volumetric flow qᵛ | 242.7 m³/h | qₘ / 998 |
| Pipe velocity V₁ | 3.615 m/s | Comfortable for water; well below erosional limits |
| Throat velocity V₂ | 10.60 m/s | V₁ / β² |
| Pipe Reynolds number Reᶠ | 5.55 × 10⁵ | Inside the machined envelope of 2×10⁵ to 1×10⁶ |
| Throat static pressure | 6.51 bar a | 7.013 bar a minus 50 kPa |
| Cavitation margin | 649 kPa | Against 2.34 kPa vapour pressure at 20 °C: no risk |
| Permanent loss at 10 % to 20 % | 5 to 10 kPa | Indicative ISO 5167-4 guidance band |
| Expanded uncertainty U (k = 2) | 1.15 % | From the budget in Table 6 |
Example 2: natural gas in an 8-inch line, and what ISO 5167-4:2022 changes
Natural gas of molar mass 17.4 kg/kmol and isentropic exponent 1.30, at 40 bar absolute and 15 °C, with compressibility Z = 0.92, in a 202.7 mm bore pipe. A machined Venturi with a 120 mm throat gives β = 0.592. The differential is 30 kPa.
This example is chosen deliberately, because the pipe Reynolds number works out at 7.95 × 10⁶, comfortably above 106. Under the 2003 edition you would have used C = 0.995 and noted that you were outside the tabulated Reynolds range. Under ISO 5167-4:2022 the correct coefficient is C = 1.000 with an expanded uncertainty of 1.8 %. The flow result changes by 0.50 %, and the uncertainty you must declare nearly doubles. Both matter, and they pull in opposite directions.
Example 2 results: 30 kPa differential, and the effect of the 2022 coefficient
Aienginear Table 9
Example 2 results: natural gas through an 8-inch machined Venturi
Showing the 2003 and 2022 discharge coefficients side by side at Reᶠ = 7.95 × 10⁶
| Quantity | Value | Note |
|---|---|---|
| Upstream density ρ₁ | 31.58 kg/m³ | p/(ZRT) with Z = 0.92 |
| Diameter ratio β | 0.5920 | 120 / 202.7 |
| Velocity-of-approach factor E | 1.0677 | 1/√(1 − β⁴) |
| Pressure ratio τ | 0.99250 | Far above the 0.75 validity limit |
| Expansibility ε | 0.99486 | Isentropic expansibility, ISO 5167-4 |
| Pipe Reynolds number Reᶠ | 7.95 × 10⁶ | Above 10⁶, so the 2022 high-Re rule applies |
| Mass flow with C = 0.995 (pre-2022) | 16.453 kg/s | 59 232 kg/h |
| Mass flow with C = 1.000 (ISO 5167-4:2022) | 16.536 kg/s | 59 530 kg/h, a 0.50 % increase |
| Normal volume flow (0 °C, 1 atm) | 76 700 Nm³/h | Reference state must always be stated |
| Standard volume flow (15 °C, 1 atm) | 80 900 Sm³/h | Same gas, different reference, 5 % apart |
| Pipe velocity V₁ | 16.15 m/s | Reasonable for gas at this pressure |
| Throat velocity V₂ | 46.07 m/s | V₁ / β² |
| Throat Mach number | 0.114 | Well below the 0.3 caution threshold |
| Critical pressure ratio | 0.546 | Operating τ of 0.993 is nowhere near choking |
| Expanded uncertainty U (k = 2) on C | 1.8 % | The 2022 high-Re value, against 1.0 % below 10⁶ |
Venturi vs orifice vs nozzle
All three are differential-pressure elements governed by the same ISO 5167 flow equation, and all three are covered by the same series. The choice between them is not about which is “best” but about which trade-off suits the duty: the Venturi buys low energy loss and tolerance of dirty service with cost, size and awkward replacement; the orifice buys cheapness and easy maintenance with a large permanent loss and a wearing edge.
Differential-pressure primary elements compared
Aienginear Table 10
Differential-pressure primary elements compared
Classical Venturi tube, Venturi nozzle and orifice plate on the attributes that decide a selection
| Attribute | Classical Venturi tube | Venturi nozzle | Orifice plate |
|---|---|---|---|
| Governing standard | ISO 5167-4 | ISO 5167-3 | ISO 5167-2 |
| Permanent pressure loss | 5 % to 20 % of Δp | 10 % to 25 % | 50 % to 80 % |
| Discharge coefficient | 0.984 to 1.000 | ~0.93 to 0.98 | ~0.60, Reynolds-dependent |
| C constant with Reynolds? | Yes, in range | Largely | No, varies with Re |
| Tolerance of dirty or abrasive fluid | Excellent | Good | Poor; the edge wears and drifts |
| Straight length needed | Short to moderate | Moderate | Long |
| Typical installed uncertainty | 0.7 % to 1.8 % | ~1 % to 2 % | 0.5 % to 1.5 % |
| Relative purchase cost | High | Medium to high | Low |
| Lifetime cost of ownership | Usually lowest on large continuous duty | Medium | Highest where energy is priced |
| Size and weight | Large | Medium | Compact |
| Ease of replacement | Difficult, a spool piece | Moderate | Easy, a plate between flanges |
| Best suited to | Large lines, energy-critical duty, slurries, short straight runs | High-velocity and high-temperature duty, steam | Small lines, low cost, frequent change of range |
Two further members of the family are worth knowing. Cone meters (ISO 5167-5) and wedge meters (ISO 5167-6) condition the flow themselves and need very little straight pipe, which makes them useful in congested plants where no Venturi will fit the available run. They cost more loss than a Venturi but far less than an orifice.
Industrial applications
The Venturi earns its place wherever flow is large, continuous and expensive to push, or where the fluid would destroy a sharp edge.
- Water and wastewater. Transmission mains, treatment plant throughput and pump station discharge. Low head loss directly reduces pumping electricity, and the smooth bore handles raw and settled water with suspended solids.
- Oil and gas. Crude, produced water and gas across gathering, processing and transmission. High-pressure gas service is exactly where the 2022 high-Reynolds coefficient becomes relevant.
- Refining and petrochemicals. Hydrocarbon and utility streams at scale, where a permanent loss on a large line is a continuous compressor or pump duty.
- LNG and cryogenics. Compression is the dominant energy cost; every kilopascal recovered reduces it. Remember to correct the throat diameter for thermal contraction at cryogenic temperature.
- Power generation. Boiler feedwater, condenser cooling water and steam. Feedwater flow is a protected measurement, so the low drift of a Venturi is valued as much as the low loss.
- Mining and minerals. Slurry lines where an orifice edge would erode within weeks. The Venturi holds its geometry and therefore its calibration.
- Pulp and paper. Stock and white water, where fibres would foul an orifice tapping.
- HVAC and district energy. Large chilled and hot water loops, where the meter runs continuously for decades.
- Food, beverage and pharmaceutical. The crevice-free, self-draining bore is straightforward to clean, inspect and validate against hygienic design expectations.
Common design mistakes
The same handful of errors account for most Venturi problems reported in the field. None of them is subtle once you know to look.
- Using the nominal pipe size as the bore. 6-inch Schedule 40 is 154.08 mm, not 152.4 mm. The 1.1 % error moves β and propagates into flow through a sensitivity coefficient greater than two.
- Sizing only at design flow. The meter is checked at maximum, found excellent, and installed. At turndown the Reynolds number drops below 2 × 10⁵ and the stated uncertainty quietly stops applying.
- Forcing β outside 0.4 to 0.7 to hit a convenient differential, then being surprised by cavitation at the low end or by tolerance sensitivity at the high end.
- Choosing the wrong type envelope. Specifying a machined convergent in a 400 mm line, or as-cast in a 60 mm line, puts the installation outside the uncalibrated rules before it is even built.
- Ignoring the 2022 high-Reynolds coefficient. Above ReD = 10⁶ a machined Venturi takes C = 1.000 and 1.8 % uncertainty. Using 0.995 and declaring 1.0 % is both slightly wrong and over-confident.
- Square-root extraction configured twice. Once in the transmitter and again in the control system. The reading looks plausible at full flow and is badly wrong everywhere else.
- Asymmetric impulse legs. Different lengths, different routing, one leg traced and the other not. This is the single most common cause of differential-pressure error in service.
- Transmitter span far wider than the operating differential, so the measurement spends its life in the least accurate part of the range.
- Treating wet steam as dry. The reading will be low, consistently, and nothing in the loop will complain.
- Quoting an uncertainty without the coverage factor. Since the 2022 revision, a bare percentage is an incomplete statement; say “1.0 % at k = 2”.
Calibration and maintenance
An uncalibrated Venturi relies on the ISO 5167-4 coefficient for its type, with the uncertainty from Table 2. That is adequate for process control, energy accounting and most plant measurement. Where it is not, the element goes to an accredited flow laboratory and is calibrated against a reference such as a gravimetric weigh tank, a master meter or a piston prover, across a Reynolds range covering the duty. The outcome is a certified coefficient and uncertainty, typically 0.1 % to 0.5 %, and that is what custody transfer requires.
The transmitter is calibrated separately, at several points across its span, keeping the square-root relationship in view: 25 % of differential span corresponds to 50 % of flow, so the points that matter for flow accuracy are clustered low in the differential range.
Maintenance protects two things, the geometry and the impulse system.
- Inspect the convergent and throat for erosion, scale and deposits. Measure the throat; flow depends on d² and a 1 % enlargement is a 2 % error.
- Record the as-built bores of both pipe and throat in the maintenance system, alongside the calibration due date, so the measurement stays traceable for the life of the plant.
- Prove the transmitter zero periodically with the manifold equalised and both isolations closed.
- Check both impulse legs for blockage, pockets, leaks and symmetry. Confirm tracing and insulation are identical on both.
- Re-verify at an interval matched to criticality and to the drift actually observed, not to a generic annual default.
Troubleshooting
Venturi meter fault-finding guide
Aienginear Table 11
Venturi meter fault-finding guide
Symptom, likely causes in order of probability, and what to check first
| Symptom | Likely causes, most probable first | Check first |
|---|---|---|
| Reads low | Wrong density or C in the flow computer; leak on the high-pressure leg; gas pocket in a liquid leg; wet steam treated as dry | Configured density and bore against the as-built data sheet |
| Reads high | Throat enlarged by erosion; wrong bore entered; liquid trapped in a gas leg adding static head | Measure the throat; compare with the as-built record |
| Reads roughly the square of what it should | Square-root extraction applied twice, or not at all | Transmitter configuration and the DCS block, together |
| Noisy or unstable | Insufficient straight length; pulsation from a reciprocating machine; two-phase flow or flashing; unequal leg lengths | Upstream piping against Table 4; look for a reciprocating source |
| Zero drifts | Unequal leg temperatures or elevations; unbalanced condensate on steam; leaking equalising valve | Seal pot levels and the manifold equaliser |
| No signal at all | Isolation valves closed; equaliser left open; blocked or frozen impulse lines | Manifold valve line-up, then tracing |
| Good at high flow, wrong at low flow | Reᶠ below the ISO limit at turndown; transmitter span too wide; low-flow cut-off set wrongly | Reᶠ at minimum flow in the calculator |
| Reading drifts over months | Throat erosion or scaling; gradual impulse line fouling; transmitter drift | Trend the zero; schedule an internal inspection |
| Audible rattle or gravel noise | Cavitation in the throat and divergent | Throat pressure against vapour pressure; reduce Δp or raise line pressure |
How this calculator compares
Aienginear Venturi Meter Calculator vs typical free online tools
Aienginear Table 12
Aienginear Venturi Meter Calculator vs typical free online tools
What most free Venturi calculators do, and what this one adds
| Capability | Typical free calculator | Aienginear Venturi Meter Calculator |
|---|---|---|
| Flow from differential pressure | Yes | Yes |
| Reverse sizing for throat diameter | Rare | Yes, bracketed solver with a round-trip check |
| Liquid, gas and steam in one interface | Usually liquid only | All three, with phase-specific checks |
| ISO 5167-4 validity envelope enforced | Seldom | D, β and Reᶠ checked per convergent type |
| ISO 5167-4:2022 high-Reynolds coefficient | Almost never | C = 1.000, U = 1.8 % above Reᶠ = 10⁶ |
| Theoretical isentropic expansibility | Often omitted or linearised | Full isentropic form with the τ ≥ 0.75 block |
| ISO GUM uncertainty budget | No | Analytical sensitivity coefficients, k = 2 |
| Cavitation margin for liquids | No | Throat pressure against vapour pressure |
| Mach number and choked-flow ceiling | No | Pressure ratio, critical ratio and throat Mach |
| Permanent loss and lifetime energy cost | No | Power, annual energy and cost against an orifice |
| Transmitter span and turndown check | No | Differential at minimum and maximum flow |
| Scenario comparison | No | Side-by-side cases retained in the session |
| Printable engineering report | No | Yes, with inputs, results, warnings and assumptions |
| Works offline, no data leaves the device | Varies | Single file, entirely in the browser, no collection |
| Cost | Free to paid | Free, no advertising, no registration |
Standards and references
Governing documents and what each is used for
Aienginear Table 13
Governing documents and what each is used for
Standards status checked October 2026; always confirm the edition named in your project specification
| Document | Scope | Role in this calculator |
|---|---|---|
| ISO 5167-1:2022 | General principles and requirements | The common flow equation, uncertainty framework, turndown guidance (Annex D) and permanent loss comparison (Annex F) |
| ISO 5167-4:2022 | Classical Venturi tubes | Discharge coefficients, validity envelopes, straight lengths, expansibility and the 2022 high-Reynolds coefficient |
| ISO 5167-2:2022 | Orifice plates | Reference point for the orifice comparison and permanent loss figures |
| ISO 5167-3:2022 | Nozzles and Venturi nozzles | Venturi nozzle coefficients where that element is selected instead |
| ISO 5167-5 / ISO 5167-6 | Cone meters / wedge meters | Alternatives where straight length is unavailable |
| ASME MFC-3M-2004 (R2025) | Orifice, nozzle and Venturi flow measurement | North American practice; reaffirmed and current |
| ASME PTC 19.5 | Flow measurement for performance testing | Acceptance and performance-test measurement |
| JCGM 100:2008 (GUM) | Expression of uncertainty in measurement | The uncertainty method: standard uncertainties, sensitivity coefficients, RSS, k = 2 |
| AGA Report No. 3 / API MPMS 14.3 | Orifice metering of natural gas | Context for gas custody transfer; governs orifices, not Venturis |
| API MPMS | Petroleum measurement | Broader custody-transfer framework |
| Crane Technical Paper 410 | Flow of fluids through valves, fittings and pipe | Pressure loss context for the surrounding pipework |
Assumptions and limitations
Stated plainly, so you know where the tool stops and engineering judgement starts.
- Single-phase, steady, full-bore flow. Wet steam, slugging two-phase flow and partially filled pipes are outside scope and are flagged rather than estimated.
- The uncertainty budget assumes ISO 5167 installation compliance. Short straight lengths, swirl, pulsation or geometry defects can exceed every contribution in the budget combined.
- Permanent loss is indicative. ISO 5167-4 presents it as design guidance, and the tool labels it accordingly rather than implying a standard value.
- Gas density uses the ideal-gas law with a user-supplied compressibility factor. At high pressure, supply a Z from a proper equation of state or a gas chromatograph, not a guess.
- Steam properties come from a correlation that tracks published steam tables closely over the common industrial range. For acceptance testing, use certified steam table values.
- Thermal expansion of the bores is not applied automatically. At cryogenic or high temperature, correct d and D yourself before entering them.
- Property data are reference values. Verify density and viscosity at your actual operating conditions.
- This is a design and checking aid. It is not sufficient on its own for custody transfer, which needs verified geometry, documented straight lengths and tolerances, surface condition and calibrated instruments under ISO 5167, ASME MFC or PTC 19.5, and the applicable AGA and API MPMS procedures.
Quick quiz: test your Venturi knowledge
1. At Reᶠ = 5 × 10⁶ through a machined convergent Venturi, which discharge coefficient does ISO 5167-4:2022 give?
2. Flow through a Venturi is proportional to which function of the differential pressure?
3. Roughly what fraction of the differential does a well-made classical Venturi lose permanently?
4. Below which pressure ratio τ = p₂/p₁ does ISO 5167 stop supporting the expansibility factor?
5. Your Venturi reads correctly at design flow but badly at 15 % flow. What do you check first?
Related Aienginear calculators and guides
The Venturi calculator sits in the Aienginear flow measurement and hydraulics family. These are the tools most often used alongside it.
Frequently asked questions
How do you calculate flow through a Venturi meter?
Apply the ISO 5167 equation qm = (C/√(1−β⁴))·ε·(π/4)d²·√(2Δpρ₁). You need the measured pipe bore D, the throat diameter d, the differential pressure, the upstream density, and the discharge coefficient for the convergent type. For liquids ε = 1; for gases and steam the expansibility must be computed from the pressure ratio and the isentropic exponent.
What is the discharge coefficient of a Venturi meter?
ISO 5167-4 gives 0.984 for an as-cast convergent, 0.995 for a machined convergent and 0.985 for a rough-welded sheet-iron convergent, each valid up to ReD = 106 or 2 × 10⁶ depending on type. Above ReD = 106 a machined convergent takes C = 1.000 with 1.8 % expanded uncertainty, a value promoted into the body of the standard in the 2022 edition.
What changed in the 2022 edition of ISO 5167?
The main points for Venturi users are the high-Reynolds coefficient of 1.000 for machined convergents, permission to use single pressure tappings, uncertainty restated explicitly as expanded uncertainty at k = 2, clarified multiple-fitting spacing, explicit flow-calibration rules, and Annex D of Part 1 recognising around 100:1 differential turndown with a modern transmitter.
Is a Venturi more accurate than an orifice plate?
Their base uncertainties are comparable when both meet their standard. The Venturi’s advantages lie elsewhere: it holds its accuracy in dirty and abrasive service where an orifice edge wears, its coefficient is constant with Reynolds number, and it wastes far less energy. An orifice is cheaper, smaller and easier to replace.
How much pressure does a Venturi meter lose?
Typically 5 % to 20 % of the measured differential, against 50 % to 80 % for an orifice plate at the same duty. The exact figure depends on the divergent half-angle and the surface finish, and ISO 5167-4 treats it as design guidance rather than a fixed value.
What beta ratio should I use?
Design into 0.4 to 0.7. Below 0.4 the throat velocity and the cavitation risk rise; above 0.7 the differential weakens and the sensitivity of flow to the throat bore climbs steeply, reaching 2.99 at β = 0.75. The ISO limits are wider than this, but the band above is where the meter behaves predictably.
How much straight pipe does a Venturi need?
Much less than an orifice, but not none. ISO 5167-4 sets the requirement by β and by the upstream fitting, from around 2.5D after a full-bore valve at low β to around 22D after multiple bends at β = 0.75. A shorter run is permitted at the cost of an additional 0.5 % uncertainty, which must be declared.
What turndown can I expect from a Venturi?
More than the old 3:1 rule of thumb suggests. ISO 5167-1:2022 Annex D recognises roughly 100:1 in differential pressure with a modern transmitter, about 10:1 in flow. The practical limit is usually the Reynolds number falling below 2 × 10⁵ at minimum flow, not the transmitter.
Can a Venturi meter handle slurry?
Yes, and it is one of the main reasons to choose one. The smooth bore and the absence of a sharp edge make it well suited to abrasive and solids-bearing service, where an orifice plate would erode and drift within weeks.
Can a Venturi measure steam?
Yes, for dry saturated or superheated steam. Wet steam is outside scope: the suspended droplets carry mass the single-phase calculation ignores, so the reading will be low. Steam service also demands condensate seal pots at equal elevation and identically traced, symmetric impulse legs.
Does meter orientation matter?
Horizontal is preferred. In a vertical line, account for the static head between the two tappings and follow the phase-specific impulse rules in Table 5. The pipe must run full in any orientation.
Why does my calculated flow differ from the plant reading?
In order of probability: the bore or density configured in the flow computer does not match reality; the transmitter zero has drifted; the impulse legs are unbalanced; square-root extraction is applied twice or not at all; or the throat has eroded. Check the configuration against the as-built data sheet before suspecting the element.
Can this calculator be used for custody transfer?
Only as a design and checking aid. Custody transfer requires a calibrated element, verified geometry and straight lengths, documented tolerances and surface condition, and calibrated instruments, under ISO 5167, ASME MFC or PTC 19.5 and the applicable AGA Report No. 3 and API MPMS procedures.
Is the Aienginear Venturi calculator ISO 5167 certified?
No, and no calculator can be. It implements the ISO 5167 equations and flags excursions outside the standard’s validity envelopes, but compliance is a property of the installation and its documentation, not of a piece of software. Treat it as a preliminary engineering and design-support tool subject to qualified engineering review.
Is my data sent anywhere?
No. The calculator is a single file that runs entirely in your browser. Nothing you enter leaves your device, nothing is stored on a server, and there is no registration, advertising or tracking in the tool.
Disclaimer
This calculator and article support preliminary engineering, screening, education and design. Discharge coefficients and expansibility follow ISO 5167; permanent pressure loss is indicative ISO 5167-4 guidance; fluid, pipe and material property data are reference values to be verified at operating conditions. Results depend entirely on the inputs and the stated assumptions. They do not replace detailed flow-measurement design, vendor data, project specifications, applicable codes or review by a qualified engineer, and they are not sufficient on their own for custody-transfer measurement. Always have critical measurements reviewed by a competent engineer before construction or operation.
Aienginear Venturi Meter Calculator · calculator v2.0.1 · article updated 20 October 2026 · standards status checked October 2026 · Published by Aienginear.com, Engineering Made Smarter. Found an error? Tell us.
Written by Muhammad Raza
Founder of Aienginear. Engineering and digital solutions professional with 26+ years managing projects, plant shutdowns and turnarounds in oil & gas, petrochemical and power generation.